Key Takeaways
- Prusa’s new HT Hotend reaches 400 °C and swaps tool‑lessly in under 60 seconds.
- It expands the Core One’s material palette to include high‑performance polymers such as ASA, PC‑Blend, PC‑Blend CF, PA11 CF, PPS‑CF, PPS‑GF, and PPA‑CF.
- Measured strength gains: +7 % inter‑layer bonding for PC‑Blend CF and +23 % pull‑out strength for PA11 CF.
- Safe use of PPS‑based filaments requires an operational air‑filtration unit because overheating can emit SO₂.
Introduction
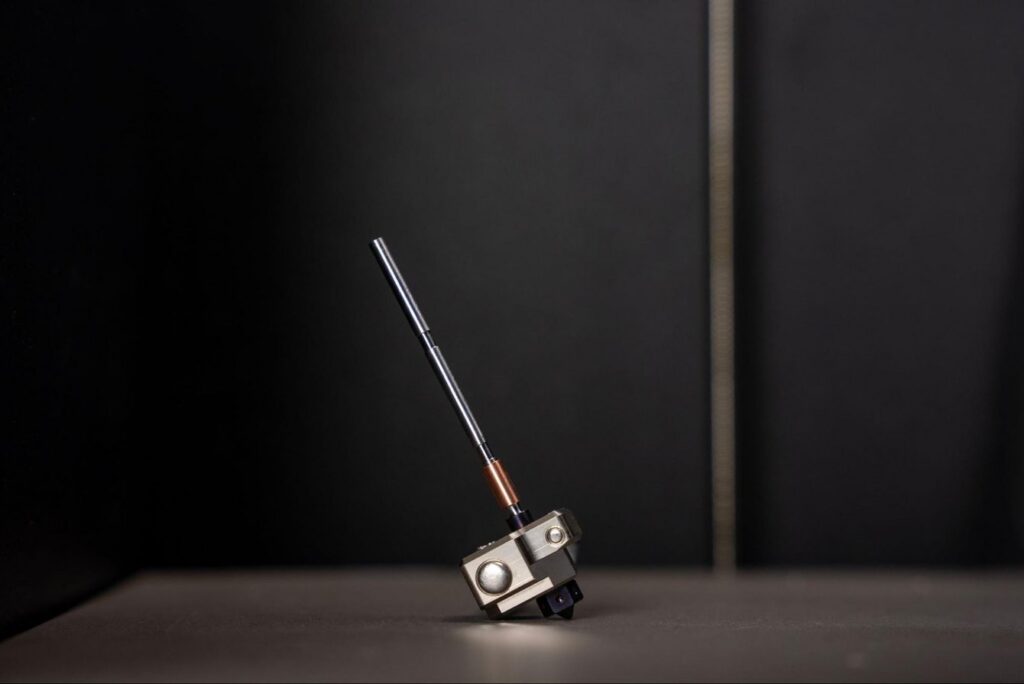
Prusa Research has launched a high‑temperature (HT) hot‑end specifically for its Core One desktop printer. Designed for rapid, tool‑free removal, the unit lets users switch between standard and high‑temp configurations in less than a minute, opening the door to a broader range of engineering‑grade thermoplastics while retaining compatibility with everyday filaments like PLA and PETG.
Technical Specifications
| Feature | Standard Core One Hot‑End | Prusa HT Hot‑End |
|---|---|---|
| Maximum Temperature | 260 °C | 400 °C |
| Nozzle Diameter Options | 0.25 mm – 0.6 mm | 0.25 mm – 0.6 mm (same range) |
| Tool‑less Swap Time | N/A (requires Allen key) | ≤ 60 s |
| Supported Materials | PLA, PETG, ABS, TPU | ASA, PC‑Blend, PC‑Blend CF, PA11 CF, PPS‑CF, PPS‑GF, PPA‑CF, plus PLA/PETG |
| Weight | 140 g | 155 g |
| Heat‑Break Material | Aluminum | Stainless steel + ceramic for thermal stability |
Temperature Range & Material Compatibility
- 400 °C capability enables extrusion of polymers with melt temperatures above 350 °C, such as PC‑Blend CF (≈ 340 °C) and PPS‑CF (≈ 360 °C).
- The nozzle’s all‑metal construction resists thermal creep, maintaining dimensional tolerance within ±0.02 mm after prolonged high‑temp operation.
Mechanical Benefits
Higher extrusion temperatures improve inter‑layer diffusion, which directly translates into stronger printed parts. Independent testing by Prusa’s R&D lab reported:
| Material | Baseline Tensile Strength (MPa) | Improvement with HT Hot‑End | Primary Gain |
|---|---|---|---|
| PC‑Blend CF | 68 | +7 % (≈ 73 MPa) | Inter‑layer bonding |
| PA11 CF | 55 | +23 % (≈ 68 MPa) | Pull‑out strength |
| ASA | 45 | +5 % (≈ 47 MPa) | Shear resistance |
The increase is most pronounced for carbon‑fiber‑reinforced blends, where the elevated temperature offsets the intrinsic reduction in intra‑layer strength caused by stiff fibers.
New Material Opportunities
PPS‑CF & PPS‑GF
- Heat Deflection Temperature (HDT): 250 °C
- UL94 V‑0 flame‑retardant rating, suitable for aerospace and automotive brackets.
- Requires active air‑filtration; overheating can release sulfur dioxide (SO₂), a health hazard.
PPA‑CF (Polyphthalamide)
- Commercially known as Zytel HTN or Ultramid.
- Drying prerequisite: 80 °C for 4 h to avoid moisture‑induced bubbling.
- Offers a balanced mix of impact resistance, UV stability, and tensile strength (~70 MPa), making it ideal for functional prototypes exposed to harsh environments.
Practical Considerations
- Filament Drying: High‑performance polymers (PA11 CF, PPA‑CF) absorb moisture; use a dedicated dryer or desiccant box.
- Print Bed Preparation: A PEI sheet or glue stick is recommended for PPS‑CF to prevent warping caused by its high shrinkage (~0.6 %).
- Cooling: Reduce part cooling to ≤ 30 % to allow proper crystallization of semi‑crystalline materials like PPS.
Comparison: Standard vs. HT Hot‑End
| Attribute               | Standard Hot‑End | HT Hot‑End |
|-------------------------|------------------|------------|
| Max Temp                | 260 °C           | 400 °C |
| Tool‑less Swap          | No               | Yes (≤ 60 s) |
| Compatible High‑Temp Filaments | None | ASA, PC‑Blend CF, PA11 CF, PPS‑CF, PPS‑GF, PPA‑CF |
| Typical Strength Gain   | N/A              | Up to +23 % |
| Recommended Filtration  | Optional         | Mandatory for PPS |
Bottom Line
Prusa’s HT Hot‑End transforms the Core One from a hobbyist workhorse into a compact, high‑temperature extrusion platform capable of handling demanding engineering polymers. The tool‑free swap mechanism minimizes downtime, while the documented strength gains—especially the 23 % pull‑out improvement for PA11 CF—justify the modest weight increase. Users who pair the HT Hot‑End with proper filament drying, bed preparation, and an active filtration system will unlock a new class of functional parts, from chemically resistant brackets to high‑strength aerospace prototypes, without leaving the desktop environment.